The adaptability of a large capacity refrigerated centrifuge wholesaler can be attributed to the many configurations and applications for which it is suited. From microcentrifuges that are used in genetic testing to heavy-duty machines for industrial processing, each is optimized for a particular purpose. The latest versions usually come with wireless monitoring systems, whose real-time data tracking occurs through mobile interfaces. Improved rotor materials allow for higher strength and corrosion resistance. In addition, automated calibration systems reduce maintenance time while improving consistency in performance. With these advancements, the large capacity refrigerated centrifuge wholesaler is a vital instrument in the continued search for scientific precision and efficiency.
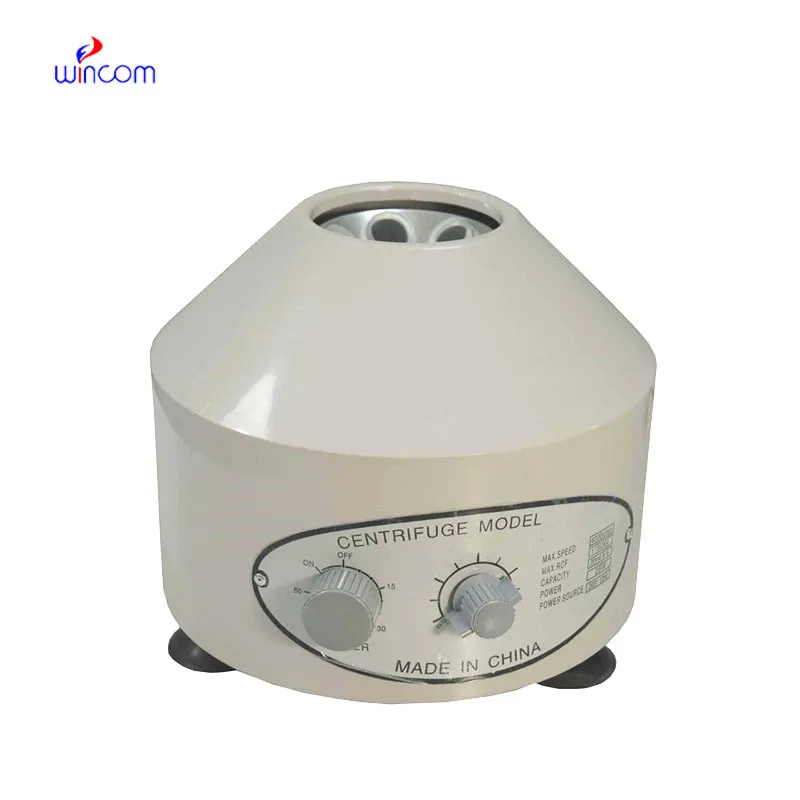
large capacity refrigerated centrifuge wholesaler are part and parcel of the functioning of modern laboratories and factories. Applications include cell culture harvesting, purification of enzymes, and waste handling. In oil processing, they facilitate hydrocarbon/water separation. Clinical laboratories depend on large capacity refrigerated centrifuge wholesaler for accurate diagnostic tests, and chemical industries use them to purify chemicals and recover active ingredients. They also hold great importance in educational research, where repetition and accuracy are necessary to experimentation. This wide application reveals the extent to which large capacity refrigerated centrifuge wholesaler continue to drive scientific and industrial advancement globally.
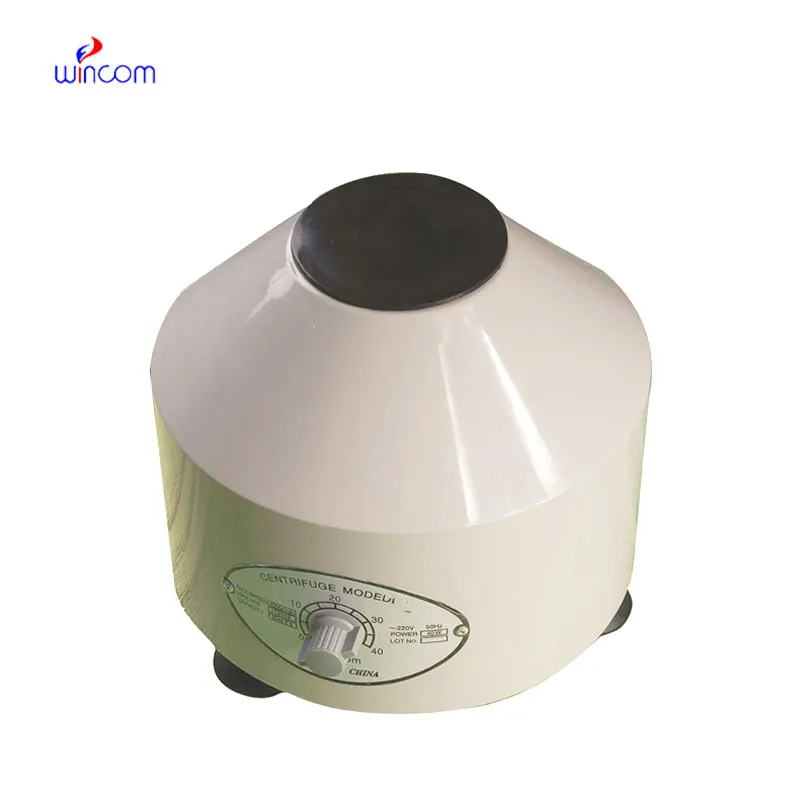
Sustainability, connectivity, and accuracy will be the areas of future evolution of large capacity refrigerated centrifuge wholesaler. Instruments will be made with sustainable materials and energy-efficient drives to minimize their carbon footprint. Real-time monitoring of data through cloud-based systems will facilitate real-time troubleshooting and process optimization. Portable versions will enhance accessibility in remote- or field-based studies. In pharma and biotech, large capacity refrigerated centrifuge wholesaler will ramp up production with intelligent automation. As technology continues to evolve, large capacity refrigerated centrifuge wholesaler will remain at the center of scientific innovation, bridging the gap between mechanical performance and digital intelligence.
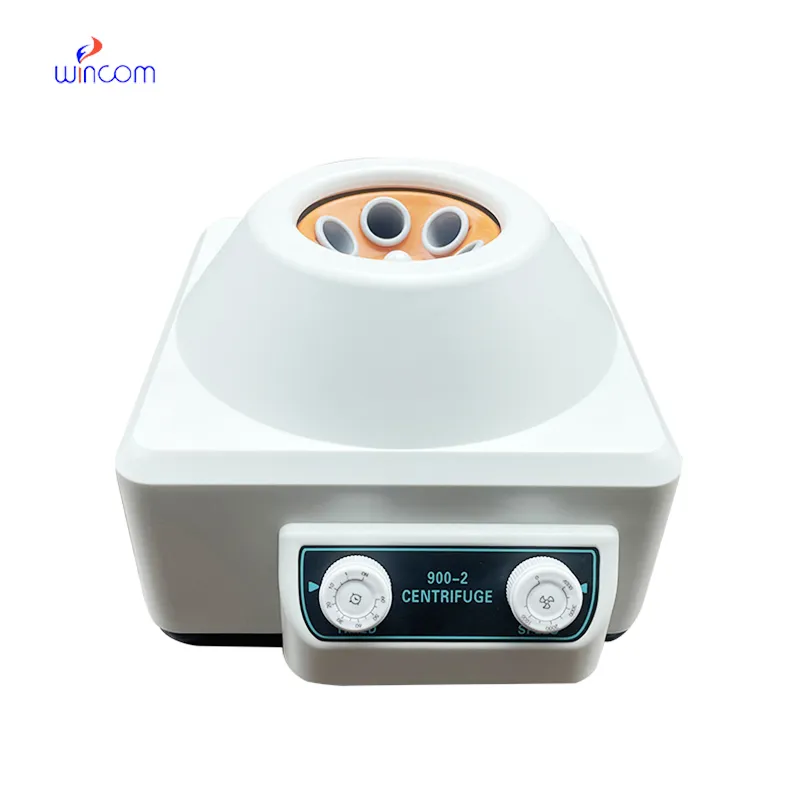
For optimal performance, large capacity refrigerated centrifuge wholesaler equipment needs to be handled cautiously and carefully. Operators need to ensure that rotors are balanced before use to avert vibration and wear. Regular cleaning of inner and outer surfaces prevents residues from building up that can impact results. Electric wiring should be inspected for loose or damaged cables. Storage of large capacity refrigerated centrifuge wholesaler in a clean, temperature-controlled environment keeps its components. Regular professional maintenance and replacement of worn parts on schedule ensure smooth and efficient use of the device over time.
large capacity refrigerated centrifuge wholesaler is a piece of mechanical equipment that separates simple mixtures into differentiated parts by utilizing quick spinning. It functions by employing centrifugal force, which expels heavier elements and brings lighter elements closer towards the axis. This principle makes crucial work possible in microbiology, pharmaceuticals, and materials science. High-speed models can achieve exceptional separation accuracy in mere minutes. Modern large capacity refrigerated centrifuge wholesaler feature digital interfaces, temperature control, and advanced safety locks to ensure operation. They are so fast and versatile that they are a must-have asset for any laboratory or manufacturing plant.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
The water bath performs consistently and maintains a stable temperature even during long experiments. It’s reliable and easy to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko